Nvidia Chief Executive Jensen Huang, wrapping up a week-long European tour that ran from the 13th through the 20th, said in Germany on the 19th that "the next wave of artificial intelligence will be technology that interacts with the physical world — manufacturing, automobiles, heavy industry and robotics." The same day, Nvidia unveiled autonomous manufacturing technology combining AI with digital twin, or virtual factory, technology at Siemens' electronics plant in Erlangen, Germany. Nvidia is jointly developing an industrial AI operating system with Siemens, aiming to raise factory automation rates from the current 30% to 40% to as much as 70% to 80%. The company sees the "brain" of a fully autonomous factory as the next growth driver in the industrial AI market.
Manufacturing AI, once limited to detecting equipment anomalies and product defects, is expanding into drawing up production plans and determining operating conditions for machinery. Going a step beyond conventional factory automation, autonomous manufacturing AI — in which the system finds its own responses to changing production conditions — has emerged as a new competitive arena in manufacturing. Where the dark factory concept focuses on removing workers from the floor to carry out predetermined tasks, autonomous manufacturing AI puts its weight on judging the optimal response each time production conditions change.
Aligning Scattered Factory Data Is the Starting Point

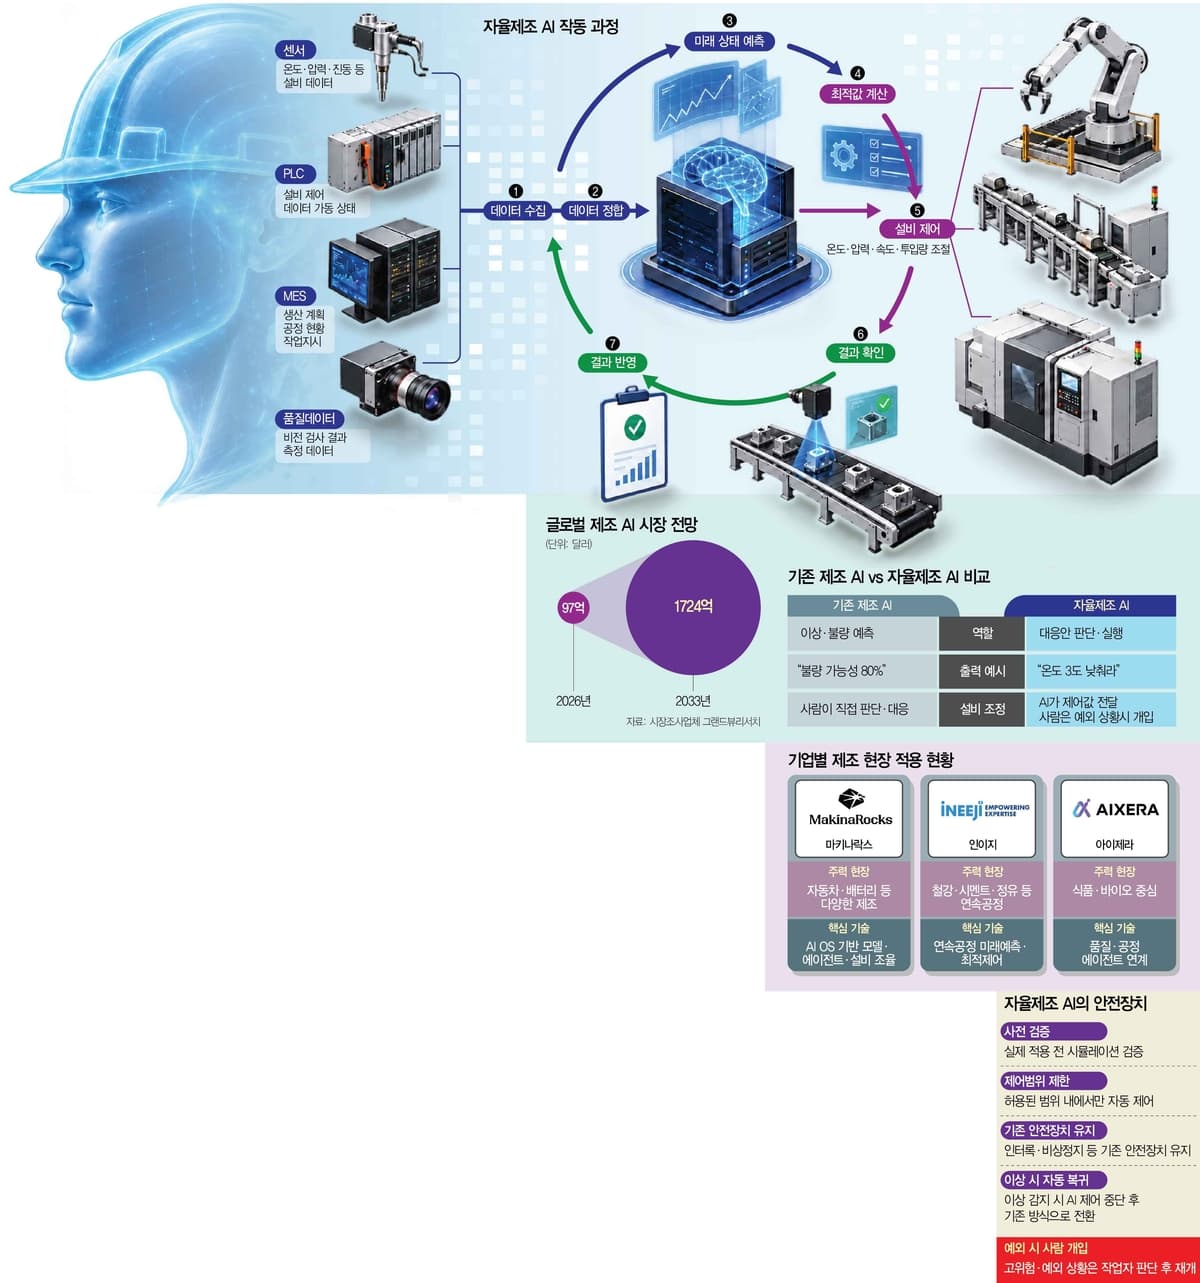
Conventional automated factory equipment simply repeated the temperatures, speeds and sequences set by humans. Even with AI added, deciding how to respond after identifying breakdown or defect risks remained a human job. Autonomous manufacturing AI grasps the changed state of the factory, predicts outcomes, then judges which operating conditions to adjust and by how much — like a veteran operator — and applies those changes to the actual equipment. Manufacturers expect demand for such technology to grow quickly as the aging and departure of skilled workers continues, since it can reduce dependence on experienced hands.
Building autonomous manufacturing AI starts with connecting data scattered across the plant under a single standard. A factory separately operates sensors measuring temperature, pressure and speed; programmable logic controllers (PLCs); enterprise resource planning (ERP) systems managing raw materials and inventory; manufacturing execution systems (MES) recording production items and work histories; and quality inspection systems. For AI to accurately grasp the state of a factory, these data sets must be integrated so that the conditions under which a product was made can be linked to how it turned out. Differing recording intervals are a particular obstacle. Sensor readings are logged by the second, while quality inspection results come only after production ends. That is why alignment technology — matching data while accounting for the time products take to move between processes and for clock discrepancies that vary by machine — matters.
Choi Jae-sik, chief executive of Innergy, a company specializing in continuous processes such as steel, cement and oil refining, said: "In the case of a furnace that heat-treats steel coils, we collect and align temperatures by zone and line speed, the steel grade, thickness and production sequence of each coil, and the final quality inspection results." He added, "Only by reflecting the time a coil takes to pass through each zone of the furnace and filtering out missing or abnormal measurements can you properly derive optimal operating conditions." Jang Sung-mook, chief executive of Aizera, which specializes in food manufacturing processes, said: "We gather data collected during the coagulation, pressing and cutting of tofu into a single time-series database and correct for clock discrepancies between machines." He stressed, "You have to calculate dwell times for each process to link raw materials, production conditions and quality results, and also pass the reliability of sensor readings to the AI, in order to prevent misjudgments."

Beyond that, the know-how of skilled workers that is never recorded in numbers must also be captured. The official permissible range for a machine can differ from the range workers judge safe based on experience. Lim Yong-seop, chief AI officer at MakinaRocks, said, "The work also involves on-site interviews to collect, in concrete terms, the criteria workers use — which machine settings they change when a particular quality indicator worsens, and beyond what level they will not make adjustments — and turning that into data." Jang also said: "In a food plant, even with the same recipe, results vary with the moisture content of soybeans, the protein content of flour, and the fat content and size of meat." He added, "What matters is turning the standards that skilled workers adjusted by feel into data, so the AI can control even fine temperature and humidity levels in the workplace according to the condition of the raw materials."
AI Derives Optimal Settings From Millions of Combinations

Once the state of the factory is understood, the next step is finding the most suitable combination among countless operating conditions. Changing one condition moves other indicators as well. Raising furnace temperature, for example, may improve steel sheet quality but also increases fuel consumption. The AI distinguishes between conditions that cannot be changed, such as raw material properties, and adjustable variables such as temperature, pressure and input volumes, then calculates optimal values while weighing quality, productivity and energy efficiency together. Testing every possible combination on actual equipment, however, is difficult. That is why companies use technology to test multiple control plans in advance inside a virtual factory trained on real plant data.
MakinaRocks has applied an AI agent to an electric vehicle battery production line using a world model-based digital twin. When the AI agent re-verifies a defect determination and judges the product to be normal, it restarts the equipment and also adjusts torque settings on the pressing device. Innergy has applied predictive control technology to the furnace of KG Steel's continuous galvanizing line (CGL). The system calculates temperature settings in advance, taking into account not only the coil currently in production but the thickness, steel grade and production sequence of the next coil, and feeds them into the actual control system.
Aizera is demonstrating technology that links quality control AI and process control AI to adjust operating conditions at Pulmuone's tofu processes. When the quality control AI analyzes deviations in coagulation state and weight, the process control AI proposes adjustments to the coagulant supply ratio or cutting conditions.
Retraining technology, which continuously reflects actual production results to maintain the AI's judgment, is also important, because predictions can go wrong as equipment ages or seasons change. Companies detect gaps between actual production results and AI predictions, along with changes in raw material and equipment conditions, to judge whether retraining is needed and update their models.
Lim said, "Retraining requires three judgments: when to do it, what data to use, and whether the retrained model is really better." He added, "We detect data drift — characteristics of data that have changed since training — and prediction errors to set the timing, and we use machine learning operations (MLOps) pipelines to apply a model on the floor only when it performs better than the existing one." Choi likewise said new models go through performance comparisons with existing models and reviews of process constraints before a decision is made on field deployment.
Safety Is the Hurdle for Wider Adoption — Protecting Lines Even When AI Errs

For autonomous manufacturing AI to take hold at more production sites, the industry says control technology must be reinforced so that a wrong AI judgment does not lead to equipment failure or a production halt. Companies are verifying control plans in advance within digital twins and building safeguards that revert to conventional control methods when something goes wrong.
Lim said, "Before a control plan is executed, we limit the values the AI can even find to within the equipment's safe range and the range workers allow, and in unfamiliar situations not seen during training, we immediately revoke the AI's control authority and switch to a mode that alerts the site manager."
Choi said: "Because the AI's judgments affect actual equipment, stricter safety principles are needed than for ordinary information services." He added, "Equipment safety functions such as the protection logic and interlocks of existing PLCs and distributed control systems (DCS) should be designed to be maintained separately from the AI, and control authority should be granted in stages according to the risk level of the process and the verification level of the AI model, in order to earn trust on the floor."