Key takeaways ▼
By Shaurya Seth
Terafab is one of the most ambitious projects of the decade: $16.8 billion for phase one and up to $119 billion across four phases. A research fab in Austin iterates on process recipes, transistor designs, and packaging variants at a few thousand wafers per month. A volume fab in Grimes County targets 100,000 wafer starts per month with first silicon targeted for 2029. Elon Musk has named Intel’s 14A as the volume process.
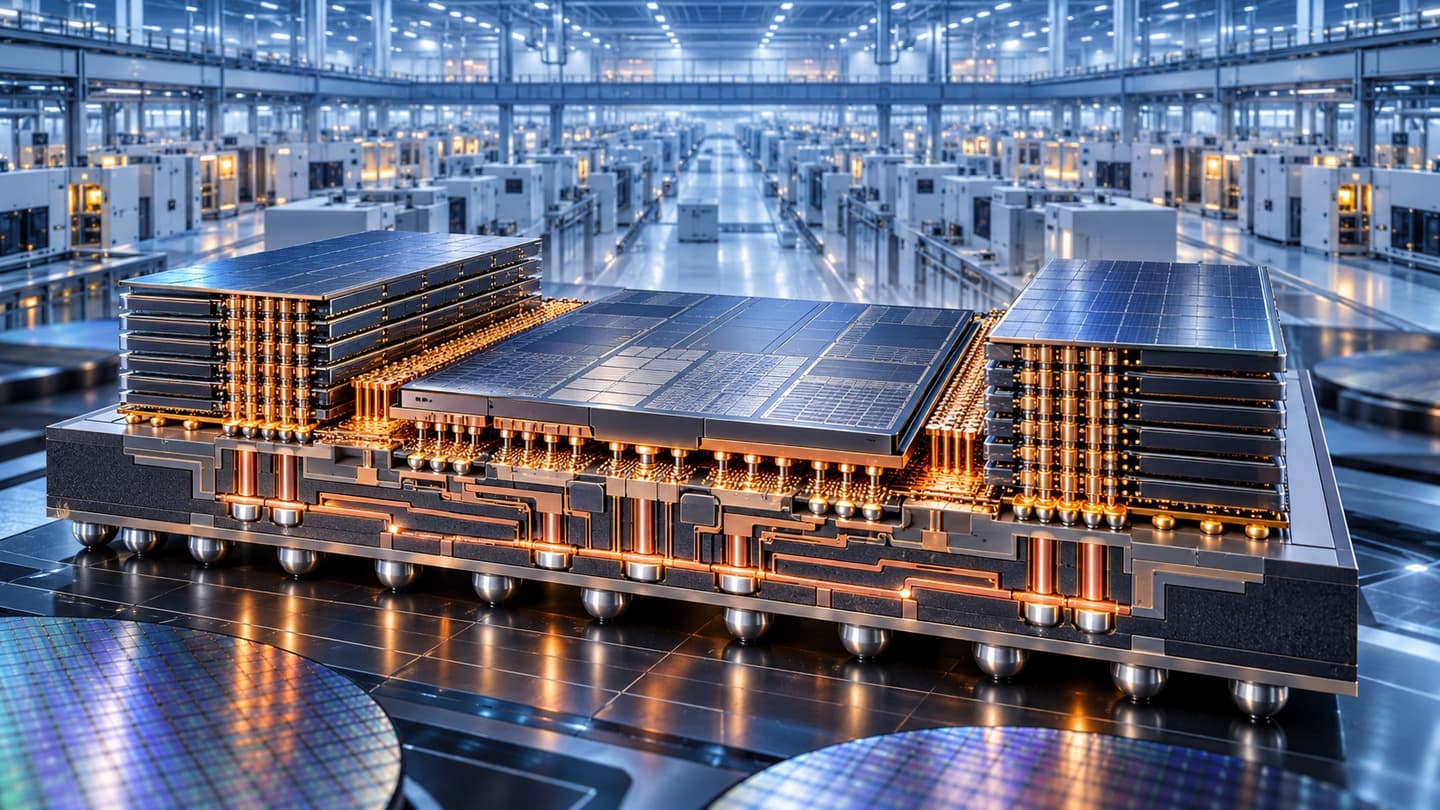
The headline claim is that logic, memory, and advanced packaging will sit under one roof. The advantage: it shortens the loop from mask revision to a packaged part, cuts Q-times between process steps, and lets one engineering organization co-design logic, memory, and package instead of separate companies negotiating process windows across time zones.
But Terafab must build from scratch an ecosystem that already exists worldwide. One roof fixes logistics but does not fix the physics inside the package. Two packaging requirements will decide whether it pays off.
Connecting HBM to Logic
HBM stacks are currently joined by Cu pillars with SnAg solder caps, using mass reflow with molded underfill (MR-MUF) or thermal compression with non-conductive film (TC-NCF). As pitch approaches 20 µm, the cap shrinks, and solder bridging becomes the main risk. The path forward is thinner caps, Sn pillars, and eventually solderless Cu-Cu hybrid bonding. My own UCLA work developed Sn pillars to replace solder bumps, targeting 10 µm pitch; 60 µm was the finest that bonded reliably die-to-wafer.
Plating sets the limits. Plating taller pillars faster means higher current density, which risks voids, rough tops, and poor within-die height uniformity; co-planarity must stay under 5%.
JEDEC’s move from a 720 to a 775 µm stack height keeps 16-high HBM4 on micro-bumps and pushes hybrid bonding to later generations, though its density, roughly 14,000 signals/mm² versus about 1,500 for TSV stacking, makes it inevitable. When it arrives, CMP becomes the largest yield variable: dielectric too high and copper never connects; copper too high and voids form. Activated surfaces also degrade while wafers wait, so Q-time becomes a yield parameter.
This is where the single roof helps. I would build Terafab’s first product as its own logic plus purchased HBM on a proven 2.5D flow, while the research fab develops hybrid bonding as one co-located CMP, activation, and bonding module with enforced Q-time limits. The catch: tool-to-tool variation. A process proven in Austin must be re-qualified to the same yield in Grimes County.
Interconnect Reliability
Once bonding works, reliability is next: these chips will run in robots and in orbit.
In 2.5D, the Sn-based joint is the weak point. As pitch shrinks, more of each joint becomes intermetallic after reflow or TCB. Cu₆Sn₅ and Cu₃Sn are brittle; as they grow and coarsen, shear strength falls with each thermal cycle until joints open. Heat accelerates that growth, and Musk says the space chips will run hotter than standard silicon. Higher current density in small bumps adds electromigration voiding. In my Sn-pillar work, die-to-wafer bonds at 60 µm pitch reached 28.26 N in shear testing. But the interfacial IMC, not time-zero strength, sets long-term behavior.
Hybrid bonding still poses risks: Cu-Cu interfaces can trap voids, and copper expands against the dielectric during anneal. My approach would be to qualify data center, Optimus, and space parts separately for thermal cycling, electromigration, and high-temperature storage; to treat Ni barriers as a trade-off between slower intermetallic growth and co-planarity; and to plan the move to nanotwinned Cu, which bonds at about 200°C instead of over 300°C.
What Would Work
Terafab’s aim is more than a terawatt of AI compute a year for Optimus, Cybercab, xAI and orbital data centers. Packaging is where that chain is least proven, so I would phase it:
- Buy proven packaging capacity first: Intel EMIB
- Bring 2.5D in-house once research-fab yields match the partner’s.
- Introduce hybrid bonding and nano-twinned Cu only when the co-located bonding module holds yield at volume.
Today, the site and phase-one funding are approved, and the research fab is under construction, but no first-wafer date or ownership terms are public, and neither Tesla nor Intel is contractually bound. One roof shortens the learning cycle; packaging decides whether it pays off.
Shaurya Seth is a Senior Process Integration Engineer at Analog Devices, where he develops BEOL processes for mature-node devices used in power electronics applications. He holds an M.S. in Materials Science and Engineering from UCLA, where his CHIPS lab thesis developed Sn electroplating for fine-pitch advanced packaging interconnects. He has published peer-reviewed research and conducted reviews for IEEE Transactions on Semiconductor Manufacturing, Journal of Applied Physics, and Materials Today Electronics.
The views, thoughts, and opinions expressed belong solely to the speaker, and not to the speaker’s employer, organization, committee or any other group or individual.
Also Read:
TSMC 2026 OIP Ecosystem Forum Summary
Data Center Energy Trends Force a Rethink of Chip Power Delivery
From Cloud to Silicon: IC-Link and TSMC Open the Door
Share this post via: